Hydraulic vs Mechanical Crimping: Which tool fits your job?
By Nicola EWN • Published: 13 Oct 2026 • 9:33 • 4 minutes read
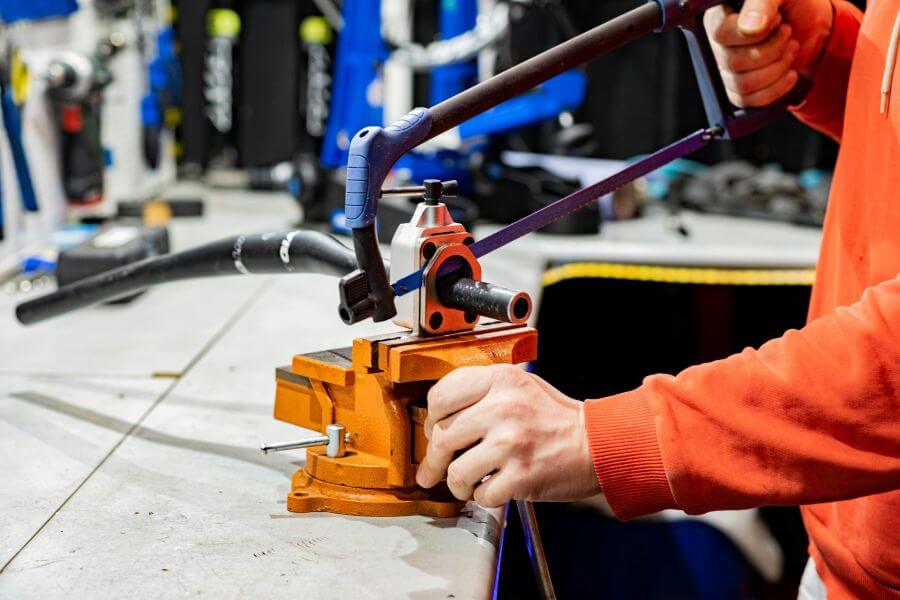
Credit: Anton Savinov/Unsplash
The choice between hydraulic vs mechanical crimping is rarely about preference and almost always about the conductor in front of you. A control panel full of ferrules and small lugs asks for one tool; a 300 mm² power connector on a switchboard feeder asks for another. Getting that match wrong shows up later as a joint that heats under load or a crimp that never reached the compression the connector was rated for, and both are expensive to find in service.
What crimping is and why it matters
Crimping deforms a connector barrel around a conductor under controlled force, creating a gas-tight interface where the two metals effectively become one continuous path for current. Done correctly, the joint holds both mechanically and electrically for the life of the installation. A termination that passes a visual check but never reached its rated compression force is the most common hidden defect in the field, because it looks finished while carrying a connection that will drift in resistance under thermal cycling. The tool is what guarantees that force is delivered consistently, which is why the method matters as much as the connector itself.
How mechanical crimping works
Mechanical crimping applies force through a hand-operated lever system, where the operator’s effort is multiplied by the tool’s mechanism and transferred to the die. It suits small cross-sections: ferrules, insulated terminals, and lugs in the low millimetre-square range, where the force required stays within what an arm can deliver repeatably. Ratcheting versions add a controlled release that prevents the tool from opening before full compression is reached, which removes one of the classic sources of an incomplete crimp. The limit is physical: as the conductor cross-section grows, the force needed climbs past what a manual lever can supply without operator fatigue compromising consistency across a working shift.
How hydraulic crimping works
Hydraulic crimping replaces muscle with a pump that drives fluid against a piston, translating modest input into compression forces that reach tens or hundreds of kilonewtons. That force is what makes large power connectors possible: cross-sections up to 300, 400, even 800 mm² are terminated with a repeatability that no manual tool can match at those sizes. The operator no longer sets the force, the tool does, which is precisely what makes hydraulic crimping the reference for high-current terminations where consistency is not negotiable. The trade-off is tool weight and cost, justified the moment the job moves into power distribution, switchgear, and feeder terminations.
Hydraulic vs Mechanical Crimping: Key differences
Force is the dividing line. Mechanical tools cover the low end where an arm suffices; hydraulic tools take over where the connector demands compression an operator cannot generate by hand. Cross-section follows directly: ferrules and small lugs on one side, power lugs and connectors on the other. Speed diverges with volume, since a mechanical tool is faster for a handful of small terminations while a hydraulic tool wins on large connectors that would otherwise take repeated manual effort. Operator fatigue is the quiet variable, because a manual tool used past its comfortable range produces crimps that degrade as the shift wears on. Repeatability is where hydraulic tools separate decisively, delivering the same force on the first connection and the five-hundredth.
When to choose each crimping method
The decision resolves on three questions: what conductor, what volume, what connector. High-count work on small cross-sections, typical of panel wiring and control cabinets, belongs to mechanical tools, where speed on repetitive small terminations outweighs everything else. Power connections on large conductors belong to hydraulic tools, non-negotiably, because the force simply cannot come from a lever. Mixed workloads, common in installation and maintenance crews that move between panel work and feeder terminations, often justify carrying both rather than forcing one tool past its range. The connector manufacturer’s rating settles any remaining doubt, since a lug specified for a given compression force defines the tool class that can deliver it.
Choosing the right hydraulic crimping tools
Once the job calls for hydraulic force, selection turns on head geometry, tonnage, and power source. Modern professional hydraulic crimping tools are battery-powered and cordless, spanning forces from around 60 kN for connectors up to 300 mm² to 132 kN and beyond for connectors up to 400 mm², with dedicated high-capacity models reaching 136 kN for conductors as large as 800 mm². Head design is a working consideration as much as a technical one: open, closed, C-head and U-head geometries, several with rotating heads, determine access in the confined space of a populated panel or a crowded cable tray. A tool that logs each crimp cycle through onboard monitoring turns crimp quality from an assumption into a record, which matters wherever terminations have to be traceable for inspection. Matching tonnage to the largest connector in the job, rather than the average, is what keeps a single tool viable across the whole installation.
Tips for a safe and reliable crimp
A sound crimp starts with the correct die matched to both connector and conductor, since a mismatched die profile voids the connection rating no matter how much force is applied. The conductor must be fully inserted into the barrel so that no strands sit outside the compression zone. Each crimp is then inspected for die-mark placement, deformation, and any sign of incomplete closure. The recurring field errors are few and consistent: wrong die, partial insertion, insufficient force from a manual tool used beyond its range, and skipped inspection on a joint that will only reveal its weakness under load.
Follow Euro Weekly News on Google News
Get breaking news from Spain, travel updates, and expat stories directly on your Google News feed.
Follow on Google NewsSign up for personalised news
Subscribe to our Euro Weekly News alerts to get the latest stories into your inbox!
By signing up, you will create a Euro Weekly News account if you don't already have one. Review our Privacy Policy for more information about our privacy practices.
Nicola EWN
Nicola is a member of the editorial team specialising in features, digital content and online publishing. With broad experience across media and communications, she works across feature articles, editorial content and digital platforms, managing content across a range of subjects.
Comments